Chemical Products Applications in Coating Industry
Chemicals serve as the core performance backbone of modern coating systems, covering four major high-performance, application-driven segments.
1. Film-Forming Resins
Polyurethane, acrylic, fluoropolymer and epoxy resins are the foundational matrix of all coatings. They form continuous, adhesive protective films on substrates, defining the basic mechanical strength, weather resistance and durability of the final coating layer.
2. Functional Pigments & Fillers
High-purity chemical pigments, graphene composite fillers and flake metal powders deliver targeted properties. They enhance corrosion resistance, block UV radiation, improve wear resistance and add specific decorative or conductive effects to the coating.
3. Processing Additives
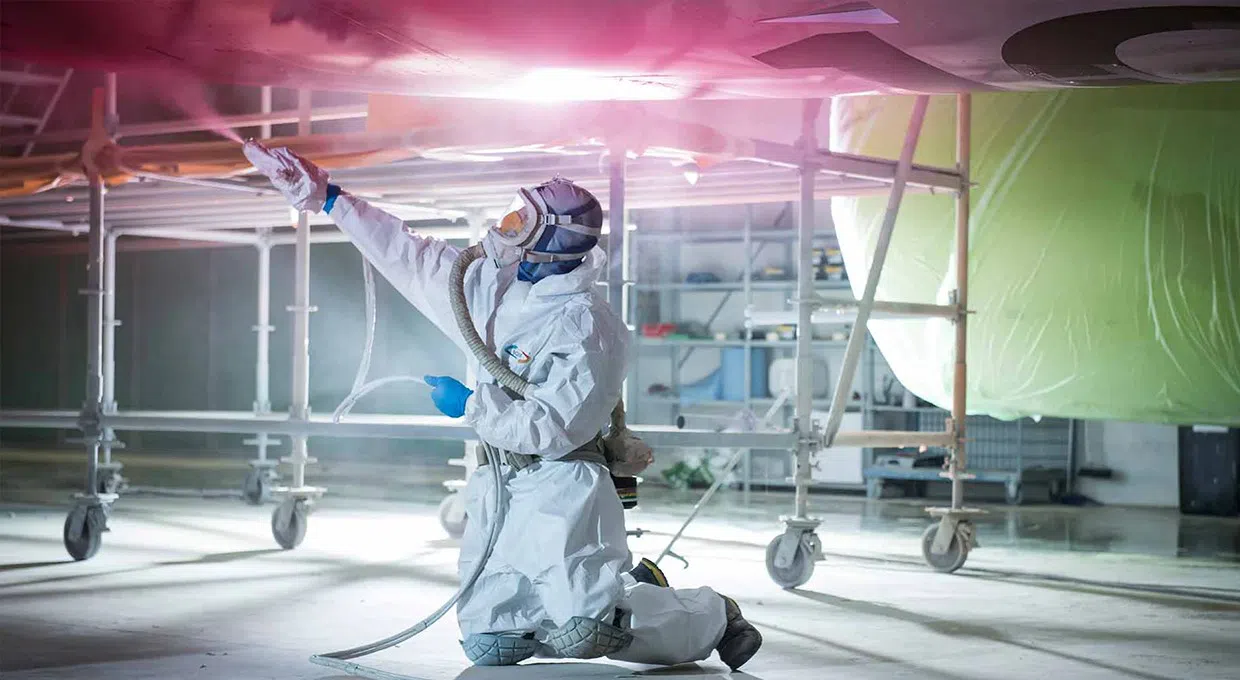
Defoamers, leveling agents, dispersants and pH regulators optimize coating manufacturing and construction performance. They eliminate surface defects, stabilize pigment dispersion and ensure smooth, uniform film formation during spraying or roller coating.
4. Environment-Friendly Solvents & Curing Agents
Low-VOC, biodegradable solvents and matched crosslinking curing agents support the shift from solvent-borne to water-based and powder coating systems. They meet strict global environmental regulations while maintaining full coating mechanical and anti-corrosion performance.
All chemical components comply with regional coating safety standards, effectively reducing harmful emissions and extending the service life of protected substrates.